Posted on: 09. 29. 26
When gas flow rates fluctuate upstream, properly designed differential pressure gas processing facilities can maintain steady throughput. Overall system resistance changes with variations in production profiles, taxing compressors and assets alike with unforeseen energy penalties. Prepare for swings in incoming flow rates by correctly sizing process equipment internals.
Natural gas flow is highly unlikely to average the same production rate across the life of a processing facility. Well depletion, seasonal demand fluctuations, and planned well shut-ins create swings in available fluid rates. Process facility equipment must flex above and below nameplate conditions to prevent downtime and efficiency losses.
Differential Pressure Gas Processing Explained | Understanding Process Swings
Differential pressure gas processing is the relationship between variable inlet flow rates and pressure loss across gas treatment equipment. If equipment is sized too small, swings in inlet flow can overwhelm vessels, causing excessive liquid carryover and high-pressure drops.
Engineers should consider maximum flow potential and minimum turndown when designing new facilities. Pressure loss through vessels is exponential to flow velocity changes. Doubling inlet flow will quadruple the friction loss experienced upstream.
| Facility Equipment | Ideal Velocity Range | Flow Swing Concern | Parameter to Size By |
| Inlet Separator | 2 to 5 ft/sec | High velocity leads to liquid entrainment | Packing and pad size |
| Filter Coalescer | 0.5 to 1.5 ft/sec | High velocities break media packing | Packing layout |
| Amine Contractor Tmn | 1 to 3 ft/sec | Low velocities lead to gas channeling | Packing height |
| Glycol Dehydrator | 1 to 2.5 ft/sec | High velocities lead to glycol dumping | Maximum design volume |
| MS Bed | 0.3 to 0.8 ft/sec | High velocities lead to dusting | Cross-sectional area |
For instance, correcting internal cross-sectional areas to match maximum throughput velocities reduces friction while maintaining gas residence time.
Baseline Gas Pressure Drop | Why You Need A Benchmark
When no gas flows through a pipe or vessel, there is zero pressure drop. Establishing a baseline gas pressure drop through equipment creates an efficiency benchmark when everything is clean, and flow rates are known.
Recording a baseline gas pressure drop when a system is first commissioned creates a valuable reference point for future engineers. With a known starting delta pressure, it’s easy to predict how much additional flow will impact overall pressure loss. But what happens when no baseline is recorded?
Without a known baseline gas pressure drop value, pumping shows will hide restrictions. Since differential pressure is directly proportional to velocity through a pipe, an operator could misidentify a normal pressure increase due to higher well counts as a plugged line. Worse yet, a reduction in gas flow may disguise fouling.
Steps to take when establishing baseline gas pressure drop guidelines include:
- Measure static inlet pressure, gas specific gravity, and temperature at a minimum of three flow rates (low, design, and high).
- Solve for the baseline coefficient of friction for every vessel and pipe segment using velocity calculations.
- Graph a continuous differential pressure over a range of flow rates curve.
With this information recorded during commissioning, operators can later automatically compute expected dP by just entering current flow rates into the control system. Any deviation from expected differential pressure is immediately recognizable as mechanical fouling.
Hydrocarbon Liquids Knockout | Why Knockout Matters to Pressure
Hydrocarbon liquids knockout refers to removing liquid hydrocarbons from the vapor phase by reducing velocity and allowing gravity to separate the heavier components. Proper vessel sizing alleviates liquid knockout concerns, ensuring liquid droplets exit the vapor phase before encountering any downstream assets.
Incoming natural gas flow first enters the separator vessel at high velocity. Mist eliminators, baffles, and cyclones slow entering gas velocities, giving droplets time to separate from the vapor phase.
Trapped Liquid Collection
Gauging proper size for these internals requires understanding how long it takes droplets to fall out of the gas stream vs. the physical footprint of the equipment. If gas enters a vessel too quickly, heavy hydrocarbons will be entrained throughout the gas flow stream. Once past vessel internals, liquid water will overload coalescing filters and burden compressor drivers.
Causes of High Pressure Drop in Gas Lines | Troubleshooting Pressure
If you are trying to determine what causes high pressure drop in gas lines, look for internal pipe build-up, hydrates, filter collapse, and oversized valves. Finding causes of high pressure drop in gas lines quickly reduces line downtime and decreases well backpressure.
High inlet flow rates will exaggerate minor vessel restrictions. Typical problems that cause high pressure loss through gas lines include:
- Hydrate Buildup: Ice-like hydrates form on the inside of pipe walls when sudden temperature decreases occur during pressure surges.
- Solid Particulates: Sand from the wellhead, corrosion byproducts, and iron oxide lodge into cool pipe surfaces or stuck filter patches.
- Wax Buildup: Heavier hydrocarbons freeze on cold pipe surfaces, creating narrow pipe pathways.
- Restriction Damage: Running control valves or orifice flanges too close to wide-open capacity causes permanent friction points.
Temperature monitoring across the entire pipe run will quickly identify causes of high pressure drop in gas lines. Large temperature drops occur when severe pipe restriction forces condensing fluids to release latent heat, otherwise known as the Joule-Thomson Effect.
Relationship Between Plant Efficiency and Pressure Drops | Leaning on Your Compressors
Every natural gas plant efficiency loss through poorly sized equipment forces compression drivers to work harder. Acceptable losses are expected through equipment but excessive plant efficiency loss increases fuel demand, reduces liquid yields, and decreases total facility production.
Whenever equipment causes a pressure drop, compressor suction pressure decreases. To maintain contracted delivery pressures, compression drivers compensate by using more fuel gas.
Quick Check | Do You Size Equipment For Swing Conditions?
Let’s see how prepared your operation is when dealing with flow swings:
- Has your facility ever seen more than a 20% increase in total gas flow since startup?
- Yes: Your filter vessels and mist eliminators should be reviewed hydraulically.
- No: Likely your system is operating within normal design velocities.
- Does your coalescer experience wildly changing differential pressures with normal production swings?
- Yes: There may be liquid entrainment or filter blocking occurring.
- No: Your filtration media may be sized correctly.
- Are you constantly throttling compressor suction valves to maintain discharge pressure?
- Yes: Poor sizing upstream is creating a large energy tax.
- No: Likely your upstream resistance is nominal.
Reach Out to Pro-Gas LLC | Let’s Talk About Your System
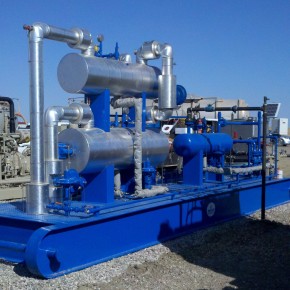
Trying to balance swings in incoming gas flow while avoiding pressure drops requires well-designed and engineered separation and fuel gas treatment equipment. Pro-Gas LLC specializes in high-performance fuel gas conditioning packages, liquid knockout units, and complete turnkey separation systems that will perform under varying turndown ratios. Our modular field skid solutions reduce pressure penalties, unload compression drivers, and keep your processing plants operating at maximum energy efficiency.
Contact Pro-Gas LLC today to speak with our engineering team about sizing equipment to fit your unique facility.
Frequently Asked Questions
Q. What are some common reasons for dP to increase across a filter vessel?
- Common issues that cause sudden differential pressure increases include liquid overload, solid particulate build-up, or hydrate formation inside the filter housing.
Q. Why does high dP cause my compressor to use more fuel?
- High dP decreases suction pressure at the compressor inlet. To keep gas flowing, the driver must use more fuel gas to reach the required delivery pressure.
Q. How much dP should I expect to see across a glycol dryer mist eliminator?
- A healthy mist eliminator will create between 0.2 and 1 PSI of dP. Anything over 2 PSI indicates significant liquid loading or hardware fouling.


